Greater China & Vietnam Newsroom
News & Insights
Language繁體中文简体中文English
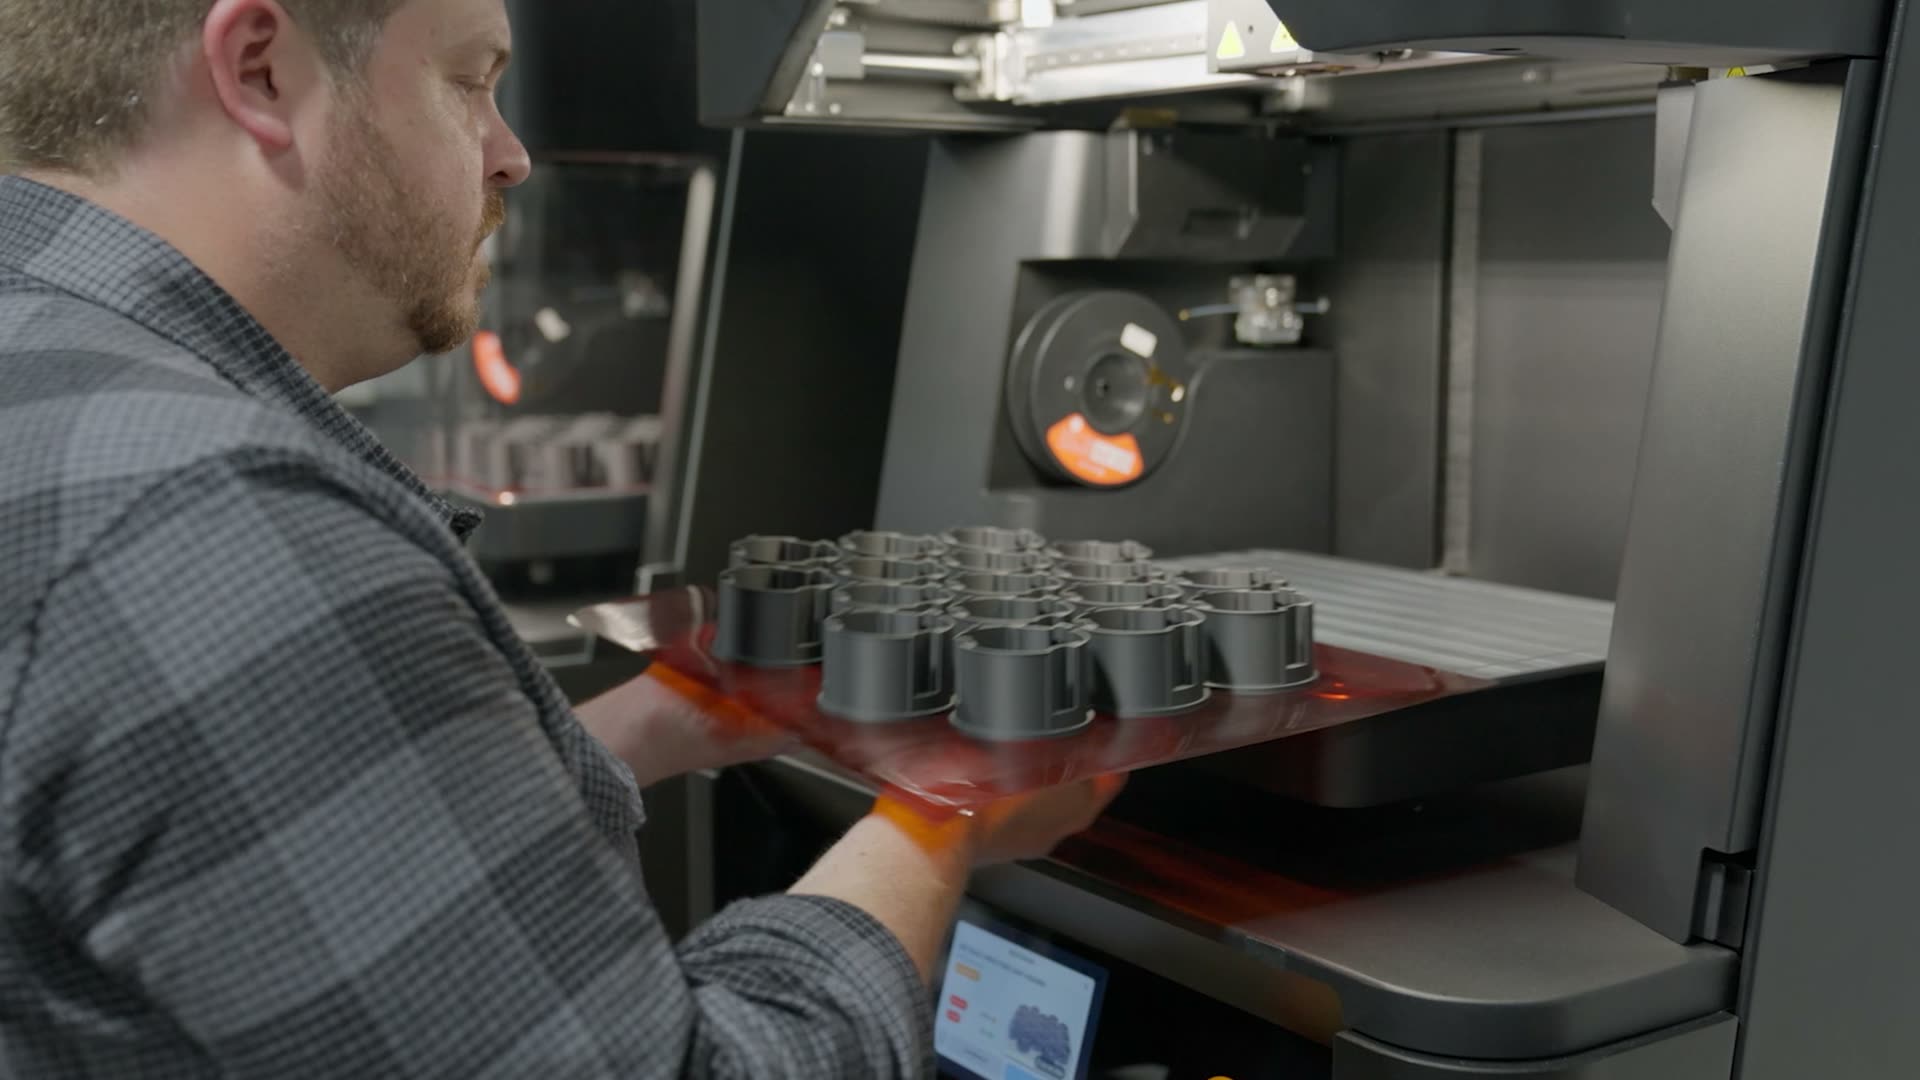
A full plate of parts coming off an FX10 (frame from an official Markforged film)
FX10 · Industrial composite + metal 3D printing

If it has to work,
it starts here.

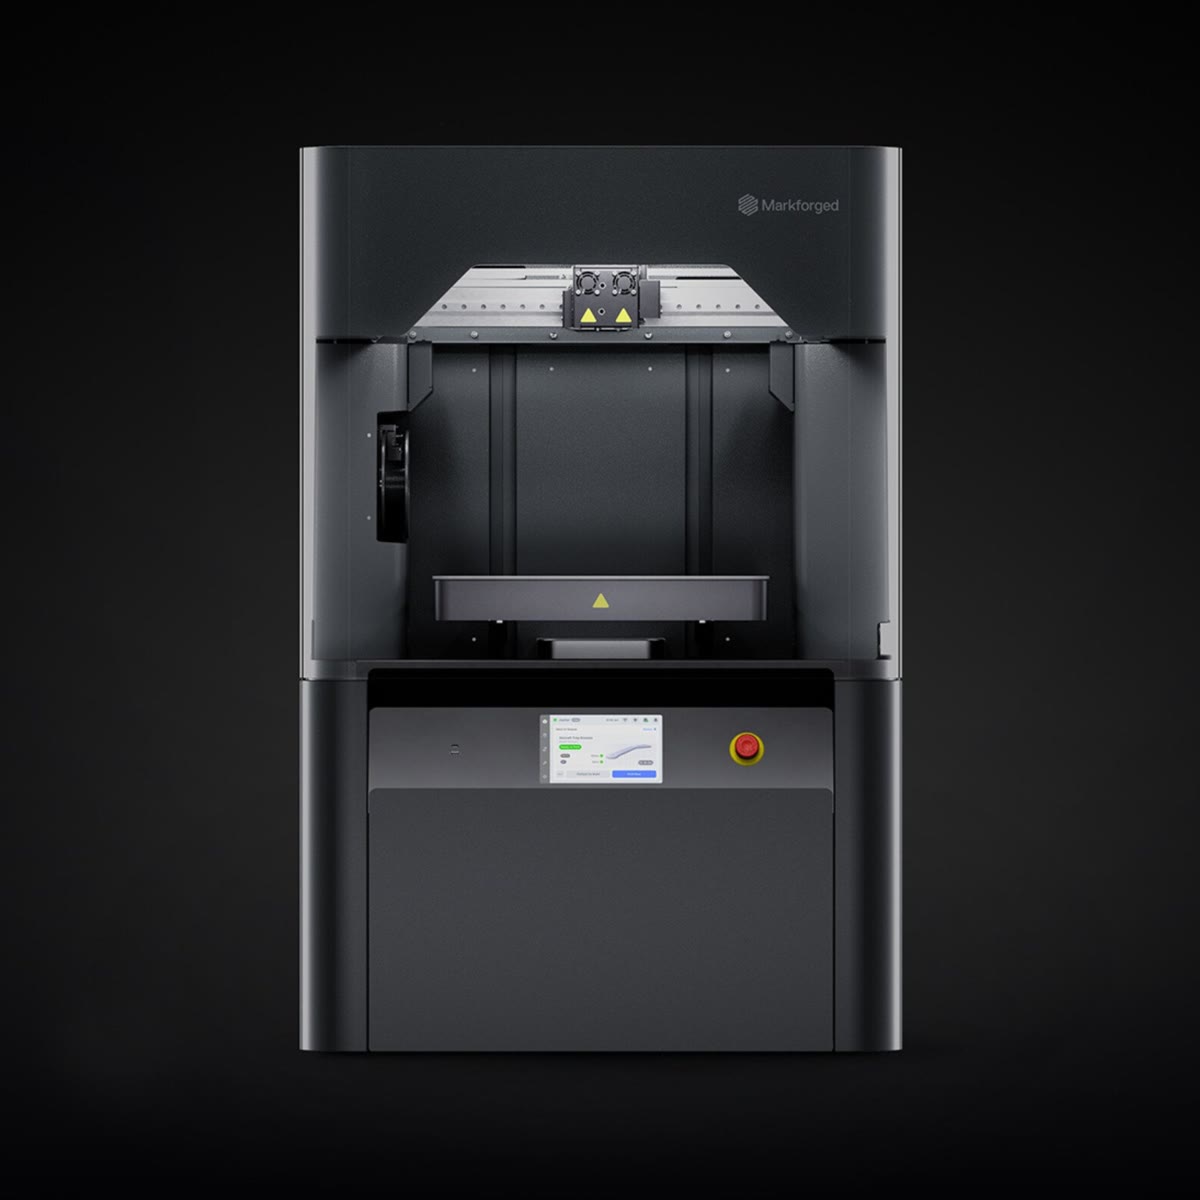
FX10 puts continuous carbon fiber composites and metal printing on one machine, on the factory floor. Fixtures printed overnight, weld-ready 316L flanges, CASA-approved helicopter ducting: all made on this machine.

FX10: one machine, two processes, right on the factory floor

Composites and metalContinuous-fiber composite fixtures and parts; swap in the Metal Kit and the same machine prints 316L, 17-4PH and H13
Measures while it printsA printhead-mounted laser micrometer scans parts during printing for dimensional checks in Inspection
Built for the floorChamber heated to 60 °C, automatic leveling and material changeover, single-phase wall power
Printer as stated in the source

Results from Markforged cases

Figures are from the original Markforged case studies; the printer is labeled as the source states it, and not every case is an FX10.

20–40 hrs → overnight
Hand-built fixtures, now designed in CAD and printed overnight
GRP · FX10
CASA approved
Bell 214B cabin ducting approved for additive production
Plane Support · FX10
−70% / −90%
Cost / lead time per fixture
Dana · X7
0.1 mm
Tolerance of Onyx GF bumper-label jigs
Subaru · printer not stated
~30 min
Manual inspection time saved per part
Hangar One · printer not stated
$244,000
Saved by one application: an out-of-production hatch plug
Fort Irwin · Markforged platform

What kind of part is yours?

Jump straight to Markforged cases with parts like yours.

01
Performance Critical.

Automotive: Performance Critical

When the line can't stop, the tooling can't fail. A supercar fabricator, a vehicle assembly plant and a global drivetrain supplier now print their own fixtures.

Official film · Automotive, Performance Critical | about 21 seconds
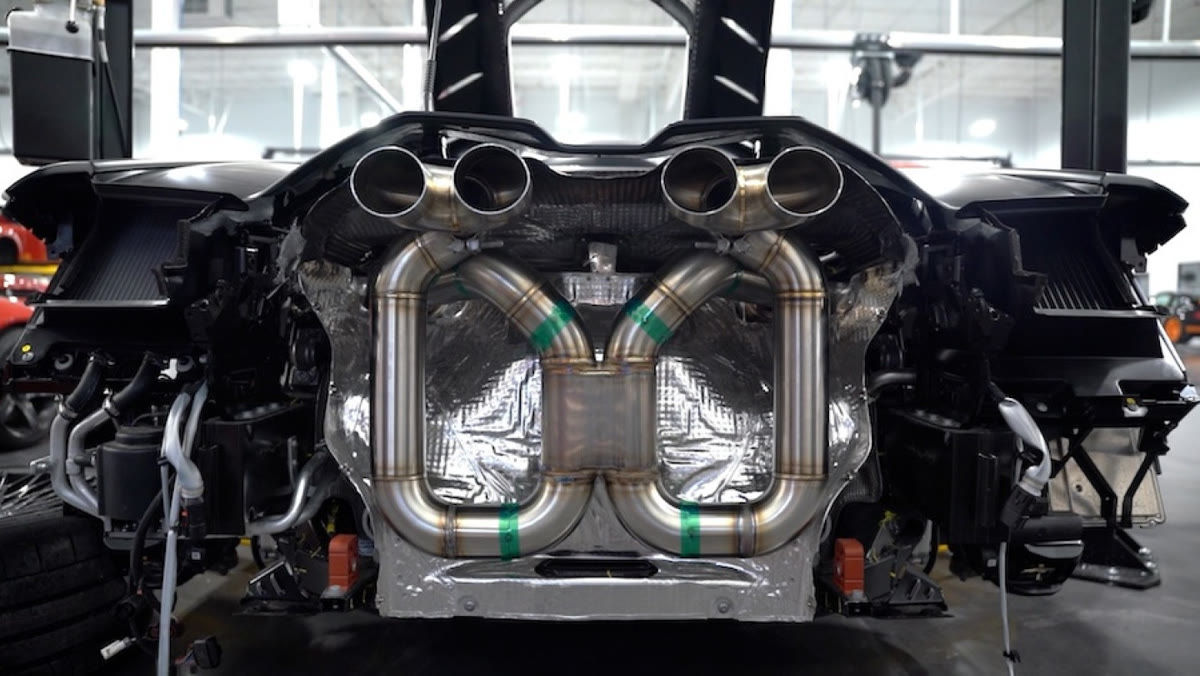
GRP's X-pipe exhaust for a Lamborghini Revuelto
FX10

Graham Rahal Performance: from 20–40 hours of hand fabrication to fixtures printed overnight

Supercar fabrication · U.S.

A fabricator used to spend 20 to 40 hours cutting, shaping and welding jigs, fixtures and exhaust components. With the FX10, they are designed in CAD, printed overnight and used the next day. For an X-pipe on the 1,000-horsepower hybrid Lamborghini Revuelto, GRP printed the flanges in 316L stainless steel on the FX10: weld-ready, with almost no post-processing.

20–40 hrs → overnightRead the original →
Assembly line at Subaru of Indiana Automotive
Printer not statedMaterial: Onyx GF (prints on FX10)

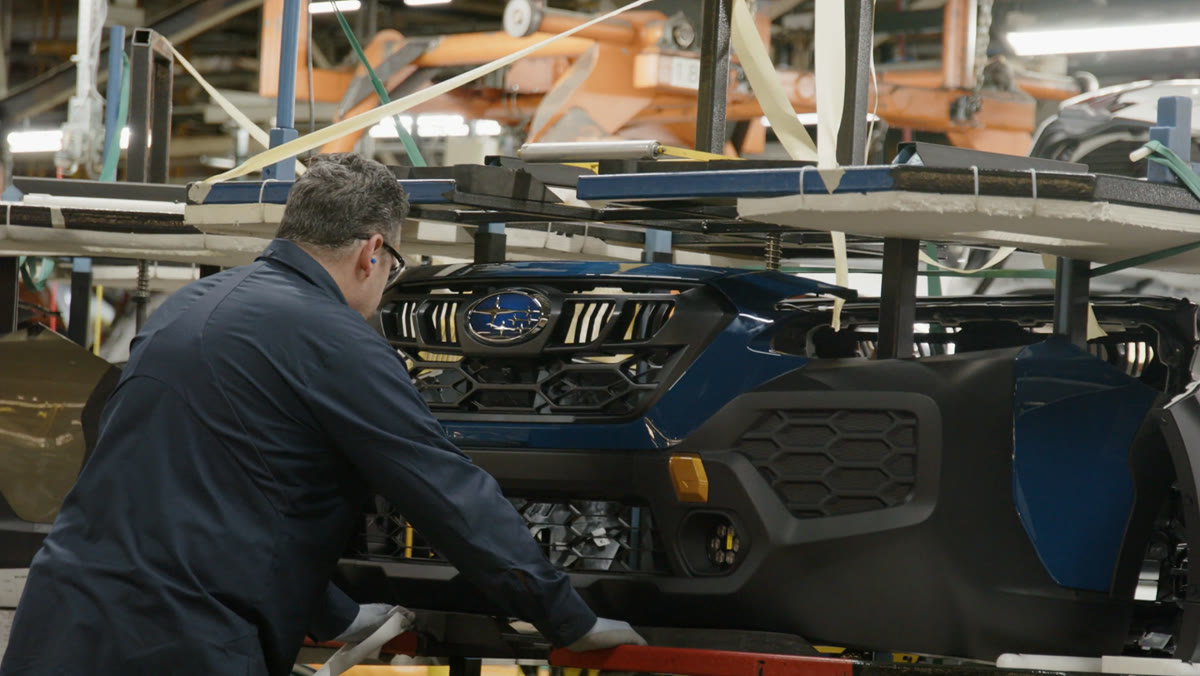
Subaru of Indiana: ABS jigs cracked, so they switched to six-color Onyx GF

Vehicle assembly · U.S.

Several models share one line and their tools differ by millimeters. Reprinted in Onyx GF, each model variant got its own color, so operators grab the right tool on the first pass; the bumper QR-label placement jigs hold a 0.1 mm tolerance.

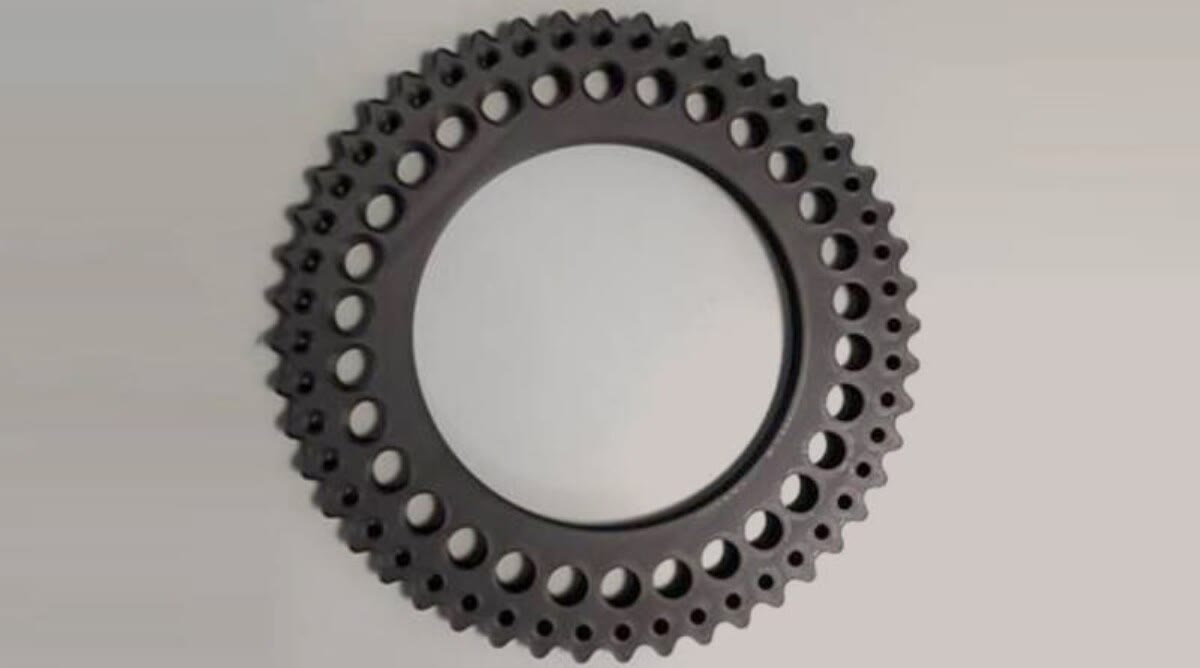
Composite workholding gear fixture printed by Dana
X7

Dana: in-house workholding fixtures, more than a year in service without failure

Drivetrain systems · Italy

Global drivetrain and power systems supplier Dana runs Markforged printers in seven countries. Composite fixtures printed on an X7 at its Rovereto, Italy engineering center ran for over a year without failure, at 70% lower cost and 90% shorter lead time per fixture.

−70% / −90%Read the original →
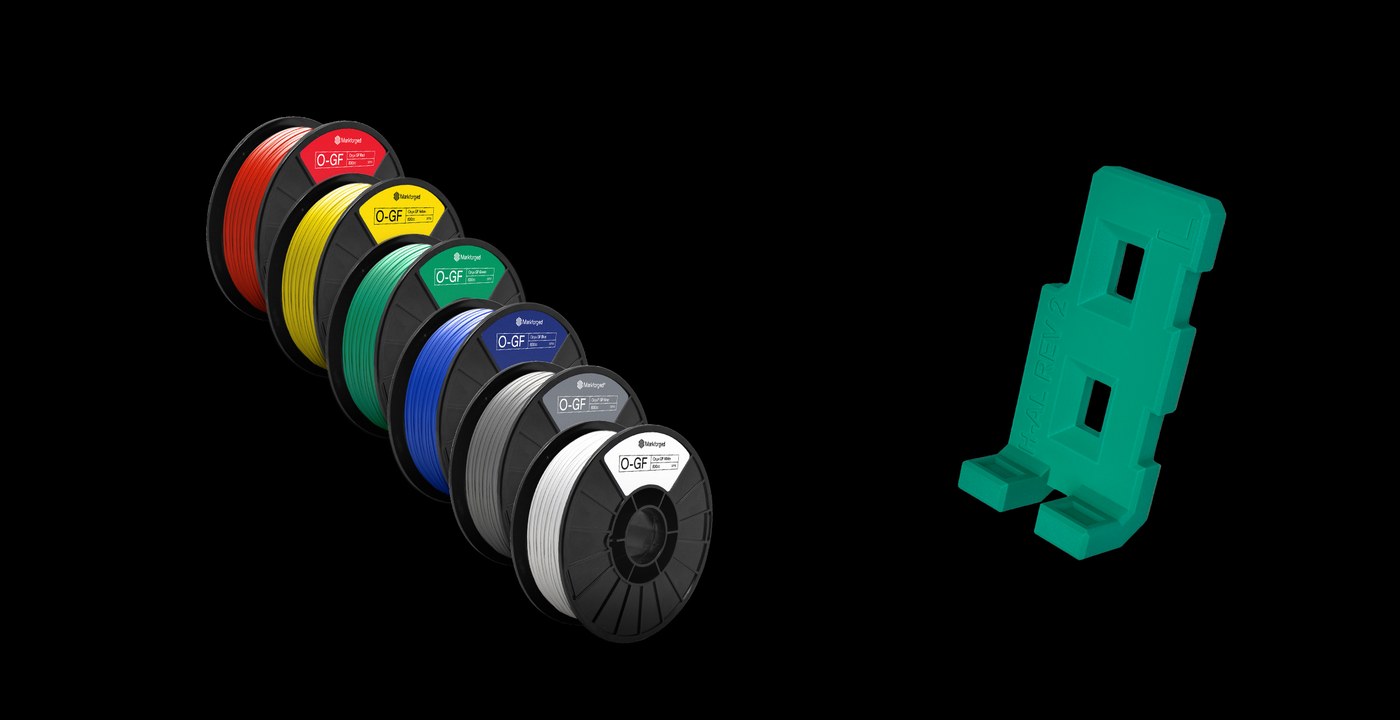
Onyx GF in six colors and a printed part (official Markforged images)
Material spotlight

Onyx GF: color is the control system

Six colors show which line, which revision and which hazard zone a fixture belongs to. Subaru of Indiana's color-coded jigs are printed in it.

Chopped-glass-fiber nylon · Non-conductive · Red, yellow, green, blue, gray, white · Continuous fiber compatible · HDT 138 °C (1.8 MPa)
Workplace safetyHigh-visibility red and yellow guards near hazardous machinery
Line differentiationTools for Line A and Line B separated by color
Revision controlNew revision, new color: old fixtures are phased out at a glance
Tool organizationA color mismatch on the shadow board shows what is missing
02
Mission Critical.

Aerospace: Mission Critical

Before it flies, every part has to pass. One shop earned CASA approval, one meets FAA requirements, and one moved inspection into the print itself.

Official film · Aerospace & Defense, Mission Critical | about 22 seconds
Bell 214B cabin ducting printed on the FX10
FX10

Plane Support: helicopter ducting printed on the FX10, approved by CASA

Helicopter engineering and MRO · Australia

Plane Support built an aerospace additive lab around the FX10 and printed Bell 214B cabin air-conditioning ducting in Onyx FR-A, a flame-retardant material with lot-level traceability. The Civil Aviation Safety Authority (CASA) approved manufacturing the part this way. Partner McDermott Aviation operates the world's largest Bell 214B fleet, used mainly for aerial firefighting.

A business jet
X7Material: Onyx FR (prints on FX10)

Cabin Management Solutions: business-jet cabin retrofits printed in flame-retardant Onyx FR

Private and business aviation · U.S.

CMS maintains, upgrades and replaces cabin management and in-flight entertainment systems for private and business jets. Founded in 2019, it bought two X7 printers and prints end-use parts such as in-flight entertainment retrofits in Onyx FR, rated UL 94 V-0, meeting Federal Aviation Administration (FAA) requirements.

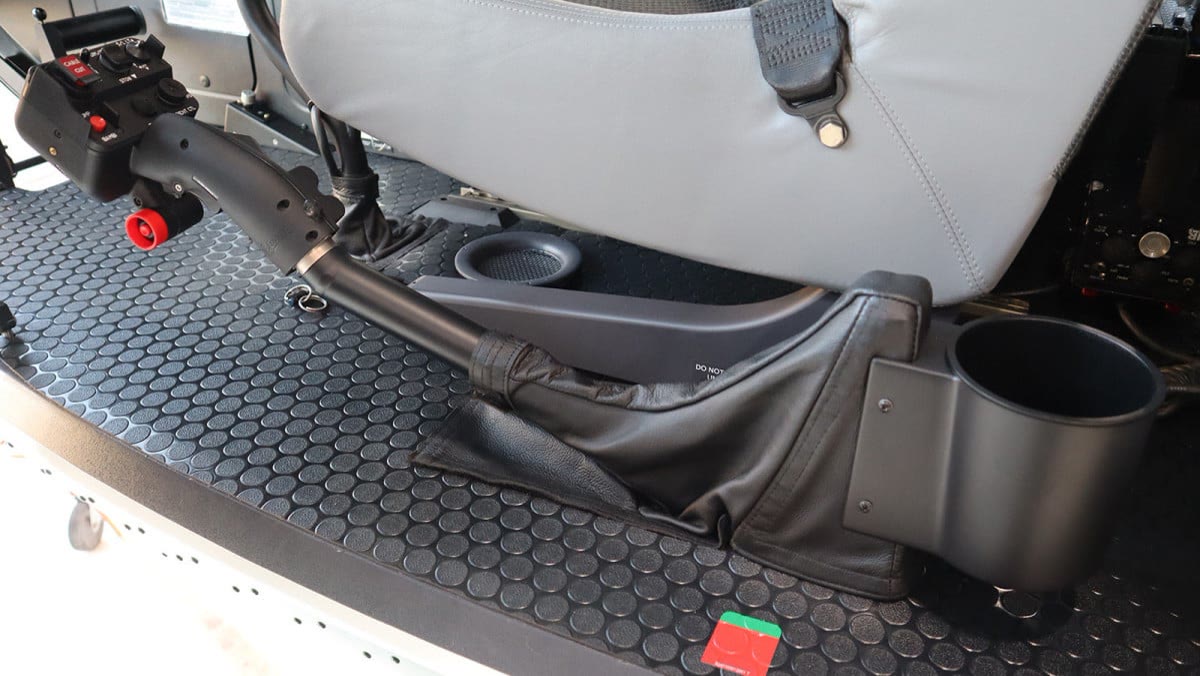
Cockpit console parts printed in composites by Hangar One
Printer not stated

Hangar One Avionics: carbon composites in place of aluminum, with inspection moved into the print

Avionics MRO and installation · U.S.

Hangar One replaces aluminum parts with carbon-reinforced composites to take weight out of helicopters, and uses Markforged Blacksmith inspection software to measure parts while they print. Manual inspection used to take 30 to 45 minutes per part; it now saves about 30 minutes per part on average.

~30 min saved per partRead the original →
03
Mission Critical.

Defense: Mission Critical

When supply lines stretch, making parts is readiness. An out-of-production hatch plug, night vision mounts broken in training, grip aids for veterans: all printed in-house.

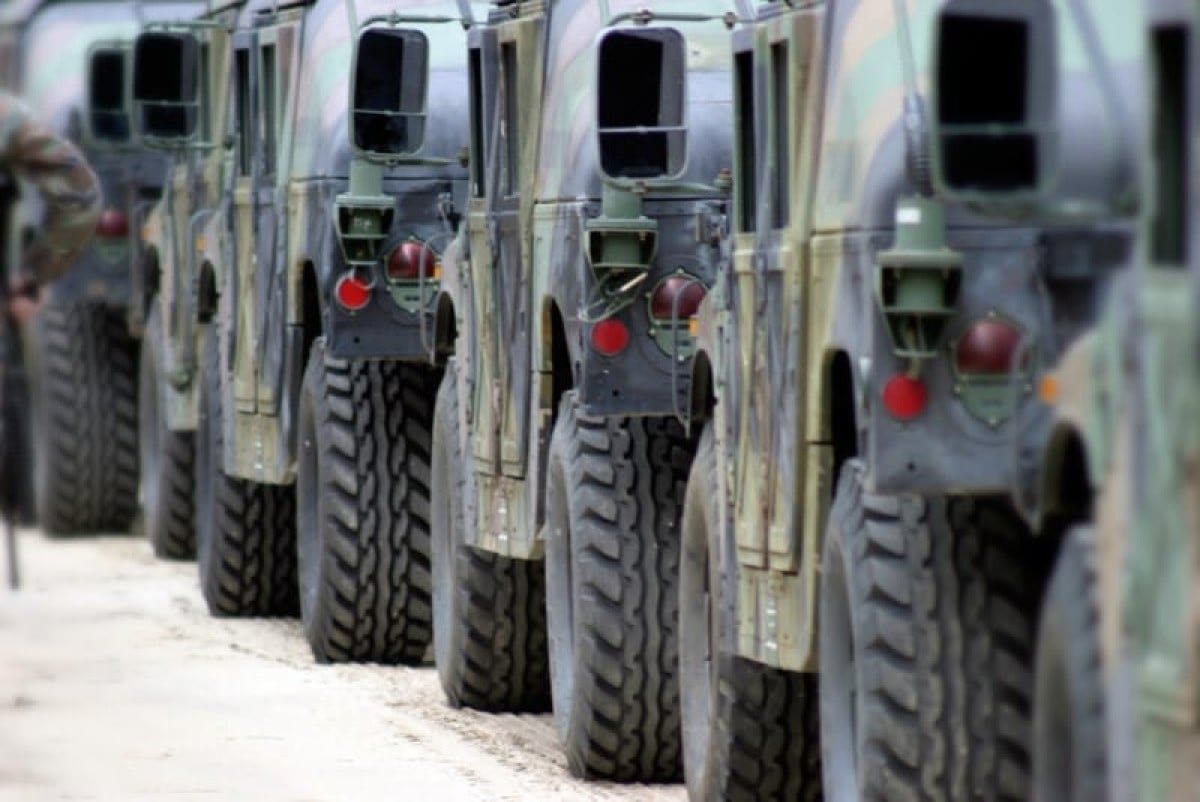
U.S. Army vehicles
Markforged platform

U.S. Army, Fort Irwin: an out-of-production hatch plug, printed back into service

National Training Center · U.S. Army

A hatch plug that helps drivers see at night was out of production; reproducing it would cost about $10,000 with a three-month lead time. The regiment printed one in Onyx for $230 and a 17-4PH stainless steel version for $800. This one application saved the regiment $244,000.

$10,000 → $230Read the original →
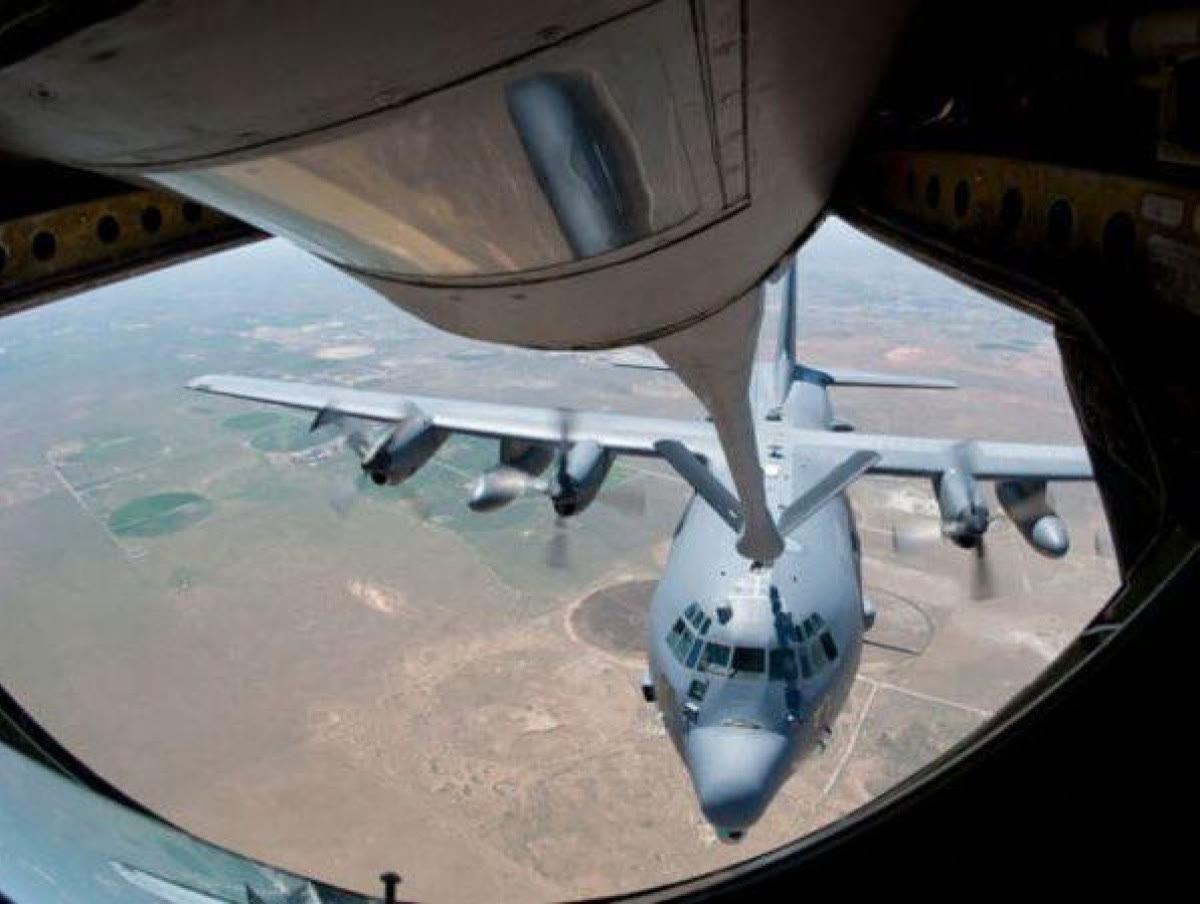
U.S. Air Force aerial refueling
X7

U.S. Air Force, Cannon AFB: night vision mounts printed in hours

27th Special Operations Support Squadron · U.S. Air Force

Night vision goggle mounts break in training, and a replacement costs $100 to several hundred dollars with weeks of shipping. The squadron printed replacements on its X7, with spacers for different helmets, for under $5 each in a few hours; the specialist in charge says they are as strong as the commercial aluminum mounts.

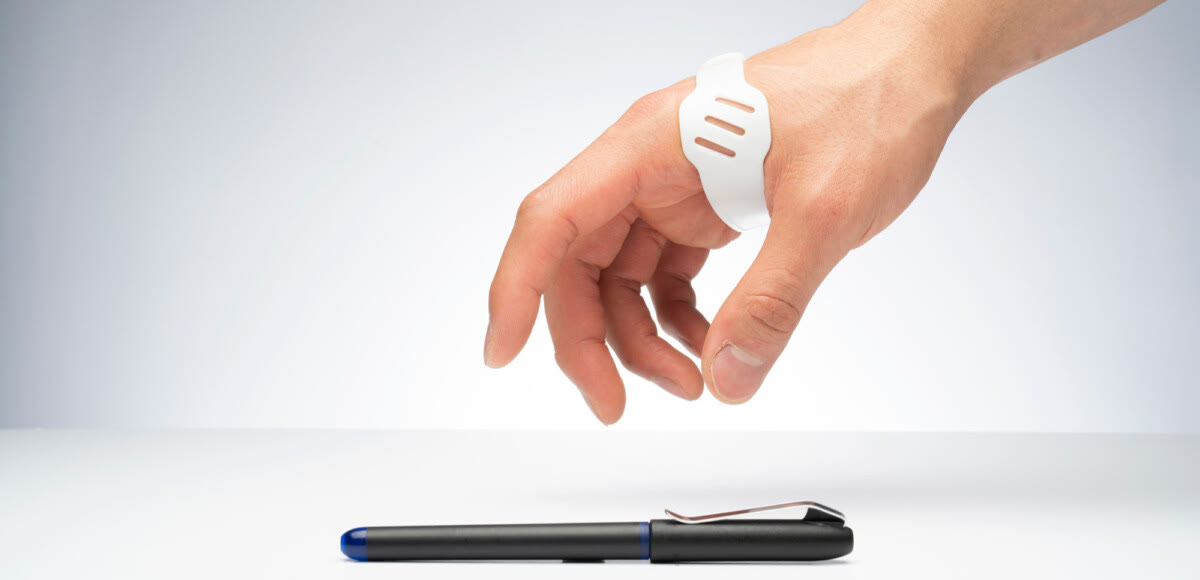
A wrist-strap stylus holder
Markforged platform

U.S. Department of Veterans Affairs: custom stylus holders for limited grip

Assistive technology · U.S. Department of Veterans Affairs

The Central Virginia assistive technology team works with occupational therapists to design a wrist-strap stylus holder for veterans and service members with limited grip, printed in flexible Smooth TPU 95A so they can hold a pen or stylus securely.

FX10 (official Markforged product photo)
Why FX10

One machine. Composites and metal.
On your floor.

Print continuous-fiber composite fixtures and parts every day; swap in the Metal Kit print engine and the same machine prints 316L and 17-4PH stainless steel and H13 tool steel, with metal parts finished in Wash-1 and Sinter-2. A printhead laser micrometer measures while it prints, with automatic leveling and material changeover that engineers and operators can both run.

FX10 at a glance

Build volume375 × 300 × 300 mm (33.8 L)
Machine size760 × 640 × 1200 mm
Build chamberHeated to 60 °C
Print bedHeated, precision-ground aluminum vacuum bed, auto leveling
Material storage4 × 800 cc spool bays, humidity controlled, automatic changeover
PowerSingle phase, wall plug
Composite materialsOnyx, Onyx FR / FR-A, Onyx ESD, Onyx GF (six colors), with continuous carbon fiber reinforcement
Metal materialsWith the Metal Kit: 316L, 17-4PH stainless steel; H13 tool steel

Need both composite and metal parts? See the FX10 Sinter-2 Bundle →

What happens next

Send a part fileWith your industry, what the part does, the material and your location
Test printWe arrange a test print of your part
Demo and quoteWe set up an FX10 demonstration and quote it

Send us the part that can't fail.

Send us a part file and we can arrange a test print and a live FX10 demonstration, and quote it. Tell us your industry, what the part does, the material you have in mind, and where you are: Taiwan, China, Hong Kong or Vietnam.

Still researching? Download the automotive e-book (PDF, 20 pages) →

Brian Chen
Your contactBrian Chen
Country Manager, Greater China and Vietnam, Markforged
For FX10 demos and quotes in Taiwan, China, Hong Kong and Vietnam, reach me directly.
brian.chen@markforged.com

Further reading